As part of the National Child Traumatic Stress Network (NCTSN), the Learning Center for Child and Adolescent Trauma offers Free Online Education with:
- 300+ FREE CE certificates
- 50+ speakers
- 200+ online webinars
- 90,000+ members
Modern production centers depend on specific chemical dealing with to maintain item quality, procedure consistency, and office safety and security. An Ultra high purity chemical delivery system is made to carry and dispense very cleansed chemicals while decreasing contamination, leak, and exposure risks. These systems are specifically vital in sectors such as semiconductor manufacturing, pharmaceuticals, biotechnology, and progressed products production. Since lots of process chemicals can be harsh, reactive, or harmful, security needs to be integrated into every phase of distribution.

One of the most essential security attributes of an Ultra high purity chemical delivery system works leak detection and control. Specialized sensing units can monitor devices locations for unforeseen chemical releases, while sealed connections and very carefully crafted piping help reduce the opportunity of leakages. Second containment structures can provide an added layer of defense by gathering unintended releases before they spread out throughout a center.
Automated alarm systems can alert operators when irregular problems are detected. Early discovery allows employees to react rapidly, isolate affected sections, and lower prospective damage to devices and workers.
Specific pressure and flow monitoring is another vital safety and security feature. An Ultra high purity chemical delivery system can integrate pressure regulatory authorities, control shutoffs, flow meters, and automated monitoring tools to maintain secure operating problems. Too much pressure might position unneeded stress on pipelines, installations, and vessels, while irregular flow can impact both safety and security and production performance.
Modern control systems can constantly check running parameters and launch safety activities when analyses move outside predefined limits. Automated shutdown features can aid protect against dangerous problems from developing into bigger occurrences.
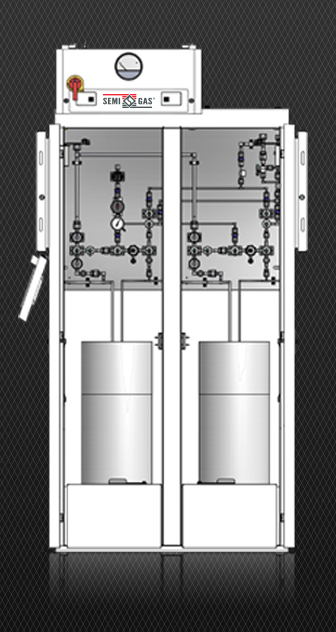
The products utilized in an Ultra high purity chemical delivery system need to be compatible with the chemicals being transported. High-grade tubing, shutoffs, seals, installations, and storage elements are selected according to chemical properties and operating conditions. Ideal product option assists reduce deterioration, degradation, bit generation, and unforeseen responses.
System honesty likewise relies on appropriate setup and maintenance. Routine inspections can identify worn seals, damaged parts, or prospective contamination points before they end up being significant problems. Keeping clean and correctly put together links is specifically vital in high-purity manufacturing settings.
Air flow systems provide an additional vital layer of security. If a chemical launch happens, effectively developed exhaust and ventilation devices can assist regulate air-borne contaminants and route them toward suitable treatment or purification systems. An Ultra high purity chemical delivery system may also incorporate encased handling locations to lower the opportunity of direct employee direct exposure.
Facilities normally integrate engineering controls with ideal operating treatments and individual safety tools. With each other, these measures aid establish numerous obstacles in between harmful chemicals and employees.
Advanced automation has considerably boosted the security of chemical delivery operations. Sensors can check stress, temperature level, flow, storage space degrees, and leakage problems in actual time. Control software application can analyze these dimensions and alert operators when unusual conditions take place.
Emergency situation shutdown systems are particularly beneficial because they can rapidly isolate chemical sources or quit delivery when a hazardous problem is discovered. Relying on center design, automated interlocks might protect against particular procedures from continuing unless required safety problems are satisfied. This minimizes dependence on hand-operated intervention throughout important circumstances. Check out this internet site https://www.chengweisemi.com/application/ about to recognize a lot more.

Innovation alone can not assure risk-free chemical handling. An Ultra high purity chemical delivery system needs regular maintenance, examination, calibration, and testing to remain reliable. Operators needs to obtain appropriate training covering system operation, chemical threats, emergency situation treatments, and contamination-control techniques.
Clear treatments for start-up, shutdown, chemical replacement, maintenance, and emergency situation feedback can additionally decrease functional threats. By incorporating robust equipment with trained personnel and regimented maintenance methods, centers can develop a much safer and even more dependable chemical delivery atmosphere.
Modern safety and security includes consequently make an Ultra high purity chemical delivery system a crucial element of sophisticated manufacturing facilities. Leak detection, automated controls, compatible products, air flow, tracking, emergency situation shutdowns, and efficient training collaborate to safeguard employees, tools, procedures, and item top quality.